Protect catalyst condition before it enters the operating vessel
Catalyst handling is often treated as a short logistics task, but the way catalyst modules are received, stored, moved, installed, and removed can affect traceability and condition. RCO catalyst elements are not interchangeable simply because their external dimensions look similar. The maintenance record should identify the approved material, module format, supplier reference, installation position, and the operating service for which it was selected.
Before delivery, request the supplier’s written instructions for packaging, orientation, lifting, moisture protection, temperature limits if applicable, shelf-life conditions if specified, and handling restrictions. Do not invent universal storage limits when the material supplier has not provided them. The site should assign responsibility for checking the shipment and preserving the instructions with the equipment records.
Review catalyst selection and compatibility →
Preserve module identity
Control storage conditions
Plan safe movement
Create traceability before shipment and installation
Receiving inspection should compare delivered labels and documentation with the purchase specification. Record module count, identification, visible shipping damage, packaging condition, and any discrepancy. If a module appears damaged or the packaging has been compromised, isolate it from normal stock and ask the supplier for a documented disposition. Do not install questionable material simply to keep a commissioning date.
Storage location should be selected according to supplier requirements and the expected time before installation. Protect the catalyst from accidental impact, unapproved contamination, water exposure, and handling by staff who do not know its restrictions. If temperature or humidity controls are specified, record how they are maintained. A generic indoor shelf is not proof that the required storage conditions have been met.
Module orientation and lifting method matter during movement. Confirm the intended lifting points, support arrangement, and restrictions on impact or twisting. Use approved lifting equipment and trained personnel, and avoid loading a module in a way that its structure was not designed to support. The handling plan should be based on the specific module instructions rather than assumptions drawn from another catalyst format.
Before installation, confirm that the vessel, supports, seals, access, and flow-direction markings match the approved drawings. Check the installation sequence and any cleanliness requirements. Keep module identities visible in the installation record, including location or layer where the design uses multiple positions. This traceability can help later diagnosis if deposits or performance changes appear in one section of the catalyst assembly.
Cleanliness should be managed without using unapproved solvents, detergents, compressed-air methods, or mechanical cleaning. A method that appears harmless to a metal surface may damage a catalyst coating or leave residues. Follow the supplier’s approved procedure and site safety requirements. If the correct method is unknown, stop and obtain written guidance rather than improvising a cleaning technique.
After installation, record the operating baseline and the conditions under which the catalyst enters service. Relevant information may include process mode, feed profile, temperature measurements, pressure behavior, instrument status, and commissioning results. The exact variables depend on the equipment. A clear baseline helps distinguish later physical damage, fouling, or chemical exposure from an initial installation issue.
During operation, keep catalyst exposure linked to process changes. New solvents, additives, cleaning agents, coating materials, or unexpected process events may alter compatibility. Operators should know which changes require engineering or supplier review. A catalyst’s original approval should not be assumed to cover every future formulation or contaminant merely because total VOC concentration remains similar.
Inspection intervals and methods should follow supplier guidance and actual service conditions. Some checks can be based on trend data, while others may require planned shutdown and physical access. Do not assume a universal catalyst replacement interval. Track pressure behavior, temperatures, process history, performance measurements, and any inspection findings that help explain the material’s service environment.
Prepare inspection and replacement without damaging evidence
Pressure drop and catalytic activity should be recorded as separate diagnostic dimensions. Deposits or damaged channels can alter flow resistance, but chemical activity loss may not create a large pressure change. Conversely, a pressure rise does not by itself prove that the catalyst has reached end of life. A service record should distinguish observed physical condition from a conclusion about catalytic performance.
| Lifecycle stage | Record or verify | Why it matters |
|---|---|---|
| Receiving | Labels, module count, packaging, damage | Confirms material matches the approved order |
| Storage | Supplier limits, location, exposure, inspection | Protects condition before installation |
| Instalasi | Position, orientation, supports, cleanliness | Preserves traceability and correct fit |
| In-service review | Feed changes, pressure, temperature, inspection | Connects performance to exposure history |
| Removal and disposition | Module identity, photos, samples, supplier decision | Supports safe reuse, replacement, or disposal |
When removal is required, plan isolation, cooling, gas testing, access control, lifting, and contamination handling under the approved site procedure. A normal dashboard reading does not prove a vessel is safe to open. The maintenance lead should confirm the equipment is in the required state and that personnel understand hazards associated with residual process material and hot surfaces.
Record the position and identity of each removed module before it leaves the vessel. Photograph visible condition where site policy permits, note deposits or damage, and keep samples tied to their original location. Avoid mixing modules from different positions or service histories in an unlabelled storage area. Preserving identity makes it easier to connect inspection findings with operating data collected before shutdown.
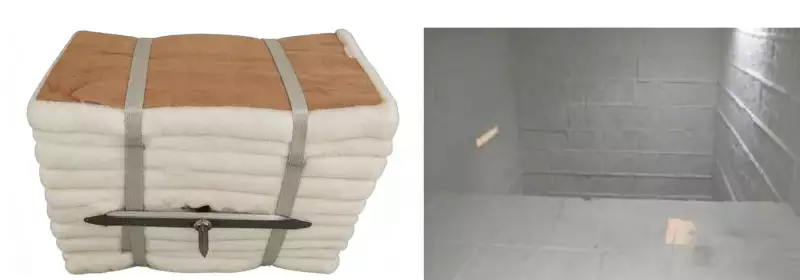
Reuse or regeneration should not be assumed possible. The decision depends on catalyst formulation, physical condition, contaminant exposure, supplier capability, and required performance. Ask the supplier what assessment is available and which criteria determine whether a module can return to service. Keep a record of the decision and the evidence behind it rather than relying on visual impression alone.
Practical review workflow
Replacement procurement should match the installed design and approved chemistry. Confirm material identity, dimensions, supports, pressure-drop basis, operating envelope, and compatibility with the actual exhaust. A part with a similar name may have a different formulation or intended duty. If the process has changed since original selection, review the new conditions before ordering a replacement set.
Spare catalyst planning should consider lead time, storage requirements, packaging, module traceability, and consequences of a planned outage. Do not order a large inventory without checking shelf conditions or assume long storage is harmless. The right strategy depends on process criticality, supplier availability, and maintenance plans. Identify who verifies spare condition before installation.
Documentation should connect purchase records, receiving inspection, storage history, installation position, operating exposure, maintenance findings, and final disposition. This record is valuable even if the catalyst performs well for years. When an issue occurs, traceable history can reveal whether a module experienced damage, unexpected exposure, or an unapproved handling event.
Review catalyst condition diagnostics →
Personnel training should cover the specific catalyst format and the boundaries of their responsibility. Operators may observe trends and record process changes, while intrusive handling may require specialist technicians. Make the approved procedure accessible at the work location and ensure lifting, isolation, and waste handling are addressed. Clear responsibilities reduce the temptation to improvise during a short shutdown.
After replacement, repeat checks required by the approved commissioning or maintenance procedure. Verify installation, instrumentation, flow path, alarms, and relevant performance baseline. If the replacement followed a catalyst-related incident, confirm that the suspected exposure source has been addressed; otherwise a new module may face the same condition. Record remaining uncertainties and schedule the agreed follow-up measurement.
Catalyst storage and handling should be treated as part of process reliability, not a warehouse detail. Correct identification, supplier-defined storage, safe movement, controlled installation, and service traceability protect both material and later diagnosis. A disciplined record also supports future procurement decisions without assuming every module has the same history.
 ID
 EN
 ZH
 ES
 AR
 PT
 FR
 JA
 RU
 DE
 MS
 CS
 BG
 NL
 KO
 RO
 SK
 TH
 VI
 ZH_TW
 UK